How to Choose a Horizontal CNC Machining Center for Die Casting Production
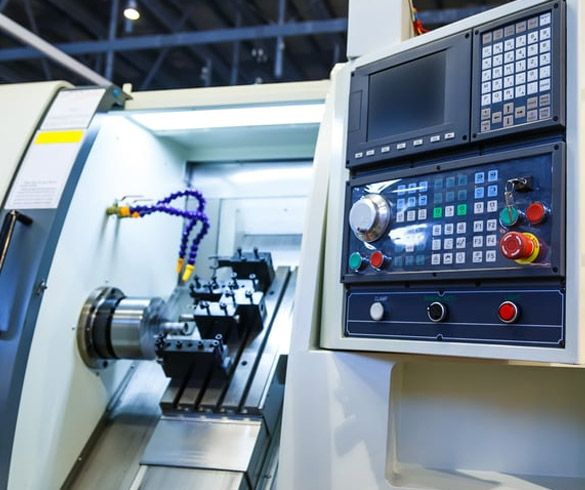
A Horizontal CNC Machining Center for die casting is a machine tool built around a horizontal spindle axis, a rotary pallet system, and a bed rigid enough to hold tolerance through long, unattended production runs. Unlike a vertical center, the horizontal spindle lets chips fall away from the fixture instead of piling on the work surface, and the pallet changer swaps parts without stopping the spindle. For die-casting shops running the same housing, bracket, or valve body thousands of times a month, that pallet-to-pallet handoff is often the difference between a machine that pays for itself and one that becomes a bottleneck. The decision tension most production managers face is not "vertical or horizontal" in the abstract — it's whether their specific casting geometry, wall thickness, and monthly volume actually justify the added cost and floor-space of a horizontal platform, or whether a vertical center with a fourth axis does the job just as well.
What Is a Horizontal CNC Machining Center for Die Casting
By definition, this is a multi-axis CNC platform designed to machine multiple faces of a die-cast part in one or two setups, using a horizontal spindle and an indexing or rotary table (often paired with a pallet pool). Die casting parts — aluminum, zinc, or magnesium — typically arrive with thin walls, cored holes, and several machined faces (mounting bosses, sealing surfaces, bearing bores) that need to stay concentric. A horizontal architecture reaches those faces without re-clamping the casting each time, which cuts cumulative fixture error and speeds up cycle time on repeat jobs. This is why the format dominates automotive, appliance, and hydraulic-fitting die-casting lines rather than one-off prototype shops.
Types of Horizontal CNC Machining Centers for Die Casting
Not every horizontal machining center is built the same way, and the differences matter more for die casting than for general fabrication. Below is a practical breakdown buyers use when comparing configurations.
| Configuration | Pallet Setup | Best Fit | Limitation |
|---|---|---|---|
| Single-pallet HMC | 1 fixed pallet | Low-to-mid volume, larger castings | Spindle idles during load/unload |
| Twin-pallet HMC | 2-station pallet changer | Mid-to-high volume repeat parts | Higher upfront cost than single pallet |
| Pallet-pool HMC | 4-10+ pallets on a pool/conveyor | Lights-out, high-volume die-casting lines | Needs larger footprint and tooling investment |
| Vertical + 4th axis | Rotary fixture on a vertical table | Smaller castings, mixed low-volume batches | Chip evacuation and multi-face access are weaker |
For buyers still comparing formats, a CNC Machining Center lineup that includes both vertical and horizontal platforms lets engineering teams pilot a part on a vertical unit before committing capital to a pallet-pool horizontal cell.
Features That Matter for Die-Casting Work
Die-cast material is abrasive and unforgiving of vibration, so the features that count are structural and control-side, not cosmetic. A cast-iron bed — commonly resin-sand cast and aged before final machining — holds geometry over years of thermal cycling better than a welded-steel frame. Ball screws and linear guideways sourced from established Taiwanese or German brands reduce backlash and keep repeat-hole positioning stable across a production shift. On the control side, look for systems with feed-forward compensation and quadrant-protrusion (quadrant-glitch) correction — these two functions are what actually eliminate the overcut marks and quadrant witness lines that show up on mold-quality die-cast surfaces. If your parts need several faces finished in one clamping, confirm the machine can complete that multi-face sequence in a single setup rather than requiring a manual re-fixture partway through the cycle.
Application Boundary — Matching Casting Size and Volume to Machine Configuration
This is the section most buyers skip, and it's the one that causes the most expensive mistakes. The right horizontal configuration depends on four linked variables: casting size, wall rigidity, fixture access, and production volume. Get any one of them wrong relative to spindle taper, pallet count, or travel, and you either overpay for capacity you don't use or bottleneck a line that needed more pallets from day one.
| Casting Profile | Wall Rigidity | Fixture Access Needed | Suggested Spindle Taper | Pallet Count | Travel Priority |
|---|---|---|---|---|---|
| Small, thin-wall (e.g., connector housings) | Low — flexes under clamp force | 2-3 faces | BT40 / CAT40 class | 1-2 pallets | Compact X/Y travel, faster rapids |
| Mid-size structural brackets | Moderate | 3-4 faces | BT40, some shops step to BT50 | 2-4 pallets | Balanced X/Y/Z, moderate Z-clearance |
| Large housings, transmission cases | High rib density needed for clamping | 4+ faces, deep pocket access | BT50 class | 4+ pallets or pallet pool | Longer Z travel, higher table load rating |
Where this format is not suitable: very small castings run in batches under a few hundred pieces a month rarely justify a pallet-pool horizontal cell — the changeover and programming overhead outweighs the cycle-time gain. Thin-wall castings with almost no rib structure also struggle on any multi-face fixture, horizontal or vertical, because the part deforms under clamp pressure before the tool ever touches it; those jobs usually need dedicated soft-jaw fixturing or a lower clamping-force setup regardless of machine choice. And if your production volume genuinely runs one or two setups a week, the capital tied up in a pallet-pool machine is better spent on tooling or a simpler single-pallet unit.
Price Factors for Horizontal CNC Machining Centers
Quoted prices swing widely because the machine is really a bundle of sub-systems, not a single line item. The main cost drivers buyers should ask about line by line:
- Pallet configuration — a twin-pallet or pallet-pool setup costs more than a single-pallet base machine but reduces idle spindle time on repeat jobs.
- Control and compensation package — feed-forward and quadrant compensation options add to the base control price but are the features that prevent scrap on mold-quality surfaces.
- Ball screw / guideway brand — Taiwanese or German precision components carry a premium over generic components but hold tolerance longer under continuous die-casting duty cycles.
- Bed casting and aging treatment — a fully aged, resin-sand cast bed adds lead time and cost but pays back in long-term rigidity and reduced re-calibration.
- Order volume — there's no hard minimum order quantity; a single unit can be purchased, but multi-unit orders typically unlock better commercial terms on pricing, lead time, or after-sales support.
- Warranty tier — standard coverage runs 12 months after acceptance with paid lifetime service afterward; some tender projects specify an extended 3-year free warranty, which is priced separately.
Typical production lead time for a configured order runs 1 to 6 months, depending on pallet count, control options, and whether the unit ships from existing stock or is built to spec.
Selection Checklist Before You Issue an RFQ
Use this checklist internally before sending drawings to any supplier:
- Have you measured casting wall thickness at the thinnest rib, not just the average?
- Do you know how many faces need machining in a single clamping — 2, 3, or 4+?
- Have you calculated real monthly volume, not theoretical capacity, for the part family?
- Does your fixture design allow tool access on all required faces without spindle interference?
- Have you confirmed whether the supplier's control includes quadrant-protrusion compensation, or only standard backlash compensation?
- Have you asked what warranty terms apply beyond the standard 12-month acceptance period?
- If your part mix changes seasonally, have you asked about customized equipment options rather than a fixed catalog configuration?
Common Mistakes Buyers Make When Specifying an HMC
- Sizing pallet count to peak-season volume instead of average monthly volume, leaving expensive capacity idle most of the year.
- Choosing spindle taper based on catalog defaults instead of the actual torque needed for the casting's rib structure.
- Ignoring fixture access review until after the machine arrives, forcing a rebuild of tooling that should have been designed against the machine's travel limits.
- Treating warranty length as a checkbox rather than confirming response time — an 8-hour response and 48-hour on-site commitment matters more on a production line than the warranty duration alone.
MAKCNC as a Horizontal CNC Machining Center Supplier
MAKCNC has operated multiple production lines since 2016 and keeps sample machines in stock, which shortens evaluation time for buyers who want to inspect a unit before specifying a full order. Our facility operates under ISO 9001:2015, and machine beds are built from high-strength cast iron with aging treatment for long-term rigidity, paired with ball screws and guideways from established Taiwanese or German brands. Control systems on our die-casting-oriented models integrate feed-forward and quadrant-protrusion compensation to address overcut marks, quadrant witness lines, and chatter — issues that show up most on mold and die-casting surface work. Machines also support multi-face machining in one setup, which suits shops running multiple part variants in smaller batches. Standard warranty runs 12 months post-acceptance with paid lifetime service, and our service network targets an 8-hour response with 48-hour on-site arrival for reported faults; select tender projects can be quoted with a 3-year free warranty on request. Buyers comparing platforms can review our global CNC machinery cases or read more about MAKCNC before requesting a formal quote.
FAQ on Horizontal CNC Machining Centers for Die Casting
Is a horizontal machine always better than a vertical one for die casting?
No. For small, low-volume castings under a few hundred pieces monthly, a vertical CNC machining center with a rotary fourth axis often reaches the required faces at lower capital cost.
What pallet count should a mid-volume die-casting line specify?
Most mid-size structural parts run efficiently on 2 to 4 pallets; scaling beyond that only pays off once monthly volume and part-family repeatability justify the added programming and tooling overhead.
Does MAKCNC offer a minimum order quantity?
No hard minimum applies — a single unit can be ordered — though multi-unit orders typically receive improved terms on price, lead time, or after-sales support.
How long does delivery take after order confirmation?
Lead time generally runs 1 to 6 months depending on pallet configuration, control options, and whether the unit is built to order or shipped from existing stock.
If you're comparing pallet counts, spindle taper, or travel specifications for a specific casting family, send your part drawings and monthly volume figures to our team for selection advice and a formal quote.