A Box Guide Vertical CNC Machining Center Controls Heavy Cut Vibration Through Sliding Contact Design
What is a Box Guide Vertical CNC Machining Center?
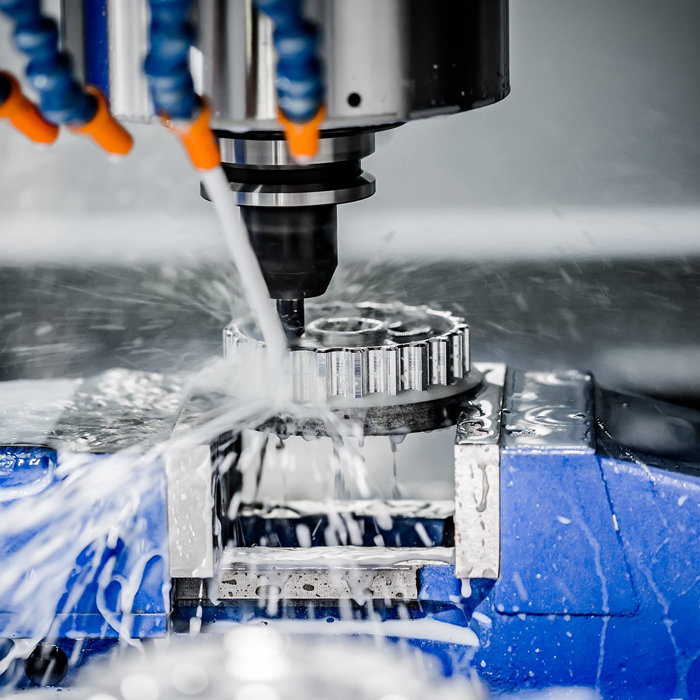
Box Guide Vertical CNC Machining Center refers to a vertical milling platform where the axis motion rides on flat, box-shaped sliding surfaces rather than round or square linear rails. The saddle and column contact each other across a broad, machined surface, not a narrow ball-bearing track. That contact area is what gives the machine its resistance to deflection during interrupted cuts, deep pocketing, or heavy face milling in tool steel and cast iron. Frames on these machines are typically built from high-strength cast iron, often resin-sand cast, and stress-relieved through aging treatment so the geometry holds over years of production, not just at the factory floor acceptance test. Buyers researching mold-and-die equipment usually land on box guide designs first, because the sliding contact directly answers the chatter problems that linear-rail machines struggle with under sustained heavy load.
Types of Box Guide Vertical CNC Machining Centers
Box guide vertical machining centers are generally sized by table travel and spindle taper, and the right size depends on part envelope more than anything else. Smaller-frame units such as the vertical cnc machining center mv970 suit mold inserts and small precision components where cycle time matters more than raw cutting force. Mid-size platforms like the vertical cnc machining center mv1160 handle general mold-base and fixture work. Larger-frame machines such as the vertical cnc machining center mv1270 and the vertical cnc machining center mv1380 extend travel for larger mold blocks and multi-cavity tooling. Shops that also need turning capacity often pair a box guide VMC with a cnc inclined bed lathe to cover shaft and disc parts on the same production line. Horizontal configurations exist too, and shops running high-volume multi-face parts sometimes prefer a horizontal cnc machining center instead, since pallet changers cut idle time on repeat batches.
How Sliding Contact, Way Geometry, and Gib Preload Create Damping
This is the part most buyers skip over during spec review, and it's the one that decides whether a machine holds tolerance at 0.3mm depth of cut or starts leaving quadrant marks and chatter lines at the same feed rate. A box guide's sliding surface distributes contact across a much wider area than a linear rail's rolling elements. That wider contact area means friction damping absorbs vibration energy before it reaches the cutting edge, instead of letting the energy bounce through low-friction ball bearings. Way geometry — whether the slide is a flat-and-vee, double-vee, or dovetail profile — determines how the machine resists torsional twist when a heavy end mill engages off-center. Gib preload, the adjustable clamping force between slide and way, controls how much play exists in that contact. Too little preload and the slide floats, producing quadrant marks on circular interpolation. Too much preload and friction rises to the point where servo motors overheat and positioning accuracy drifts over a shift.
| Parameter | What It Actually Controls | Consequence If Set Wrong |
|---|---|---|
| Sliding contact area | Damping of vibration energy during interrupted cuts | Too small an area: chatter marks, tool wear, poor surface finish |
| Way geometry (vee/dovetail/flat) | Resistance to torsional twist under off-center loading | Wrong profile for load direction: uneven wear, accuracy loss on one axis |
| Gib preload | Play between slide and way, friction level | Too loose: quadrant marks. Too tight: motor overheating, drift |
| Lubrication film thickness | Balance between stick-slip and excess friction | Wrong viscosity: stick-slip at low feed, or overheating at high feed |
Advanced control systems on production-grade box guide machines add intelligent feedforward compensation and quadrant-spike correction to work alongside the mechanical damping, targeting exactly the "overcut marks, quadrant marks, chatter lines" trio that mold shops complain about most. Mechanical damping and control-side compensation aren't substitutes for each other — a machine with poor way geometry can't be fully corrected by software, and a machine with excellent geometry still benefits from feedforward tuning on tight-radius mold contours.
Box Guide Vertical CNC Machining Center Applications
These machines fit best where cutting force is high and part geometry demands multiple operations without repositioning. Mold and die shops use box guide VMCs for cavity roughing and semi-finishing in P20 and H13 steel, where sustained radial load would push a linear-rail machine into visible tool marks. Aerospace bracket producers use them for deep-pocket milling in aluminum and titanium billet. Job shops running multi-variety, small-batch work benefit from single-setup, multi-face machining capability, since fixturing time often costs more than spindle time on short-run parts. Where a job doesn't fit a standard frame — oversized fixtures, non-standard table layouts, custom tool changers — customized CNC machining solutions extend the same box guide platform to match the part rather than forcing the part to fit a catalog machine. Applications outside heavy milling, such as light-duty engraving or high-speed small-part production, generally don't need box guides at all; linear-rail machines run faster in those cases and box way damping brings no benefit worth the tradeoff in rapid traverse speed.
Box Guide Vertical CNC Machining Center Price
Pricing on a box guide vertical machining center moves with frame size, spindle taper, control brand, and the origin of the ballscrew and rail components. Machines using Taiwan or German-brand precision ballscrews and guideways sit at a higher price point than machines using domestic components, but they hold accuracy longer under continuous heavy cutting — a factor worth weighing against upfront cost for shops running two or three shifts. There's no fixed minimum order quantity; a single unit can be purchased, though batch orders of multiple machines typically unlock better pricing, delivery scheduling, or after-sales terms. Lead time generally runs one to six months depending on configuration and current production queue.
| Cost Driver | Impact on Price | Buyer Consideration |
|---|---|---|
| Frame size / table travel | Larger frame = higher base price | Match to largest part, not average part |
| Ballscrew / rail brand | Premium brands add 10-25% typically | Justified for high-duty-cycle shops |
| Control system | Feedforward/quadrant compensation adds cost | Worth it for mold cavity work |
| Order volume | Multi-unit orders improve terms | Consolidate purchases where possible |
Box Guide VMC User Guide and Common Setup Mistakes
Getting stable performance out of a box guide vertical machining center is mostly about respecting the run-in period and keeping lubrication consistent. Follow this sequence when commissioning a new machine:
- Level the machine on isolation pads before bolting to the floor — an unlevel base transfers stress into the box ways over time.
- Run a 24-48 hour break-in cycle at reduced feed to let the sliding surfaces seat against each other.
- Check gib preload with a feeler gauge after the first 100 operating hours, since new surfaces settle slightly.
- Verify way lubrication delivery at every travel point, not just at the home position.
- Re-check squareness and backlash after the first heavy-cut job, before running a full production batch.
Common mistakes we see reported from the field:
- Skipping the break-in cycle and running full-depth cuts on day one, which accelerates way wear.
- Using the wrong lubricant viscosity, causing stick-slip marks at low feed rates.
- Ignoring gib adjustment for months, letting play accumulate until quadrant marks appear on circular work.
- Positioning the machine near a punch press or stamping line without vibration isolation, which defeats the box way's own damping advantage.
Choosing a Box Guide Vertical CNC Machining Center Supplier
MAKCNC has manufactured CNC lathes and machining centers since 2016 across multiple production lines, with demo machines kept in stock for buyers who want to inspect a unit before committing to a full order. Our facility operates under ISO9001:2015, and standard warranty runs 12 months after acceptance, with paid lifetime service support afterward — some tender-based projects qualify for extended three-year free warranty terms. Our service network targets an 8-hour response and 48-hour on-site arrival for breakdown support, which matters more than most spec sheets once a machine is running production. Shops evaluating a heavy-cut mold or die project can review documented deployments on our global CNC machinery cases page, or compare turning options through our high quality and durable cnc lathe lineup if the job needs both milling and turning capability. Background on our manufacturing scope is available on the about MAKCNC page.
FAQ of Box Guide Vertical CNC Machining Centers
Does a box guide VMC run slower than a linear-rail machine?
Rapid traverse is generally lower on box guide machines because sliding friction is higher than rolling-element friction on linear rail systems. That's the tradeoff for the added damping — shops running light aluminum parts at high speed often prefer linear rails, while heavy steel milling favors box ways.
How often does gib preload need adjustment?
Check at 100 hours after commissioning, then roughly every six months under normal duty, or sooner if quadrant marks start appearing on circular cuts.
Can a box guide machine handle mold cavity finishing, not just roughing?
Yes, when paired with feedforward and quadrant-spike compensation in the control system. The mechanical damping handles roughing loads; the control compensation refines finishing passes on contoured surfaces.
Is there a minimum order quantity?
No hard minimum — single units are available. Multi-unit orders typically get better pricing and delivery terms.
What certifications does MAKCNC hold?
Our production facility is ISO9001:2015 certified.
If you're evaluating a box guide vertical machining center for a heavy-cut mold or die application, send us your part drawings or spindle load requirements and we'll help match the right frame size and configuration.