Automatic CNC Turning Lathe Automation Options Deserve a Closer Comparison Before You Buy
An Automatic CNC Turning Lathe is a turning machine built to load, cut, and unload parts with minimal manual handling, using bar feeders, loaders, or robotic systems instead of an operator placing each blank by hand. The decision isn't whether to automate — most repeat-part shops already know they need to. The real tension is which loading hardware fits your stock format, batch size, and labor budget. Pick the wrong configuration and you either overspend on a robot cell for simple bar work, or bottleneck a high-mix shop with a feeder that can't handle part changeovers. This guide breaks down the six most common automation setups so you can match hardware to your actual production pattern before requesting a quotation.
What Is an Automatic CNC Turning Lathe?
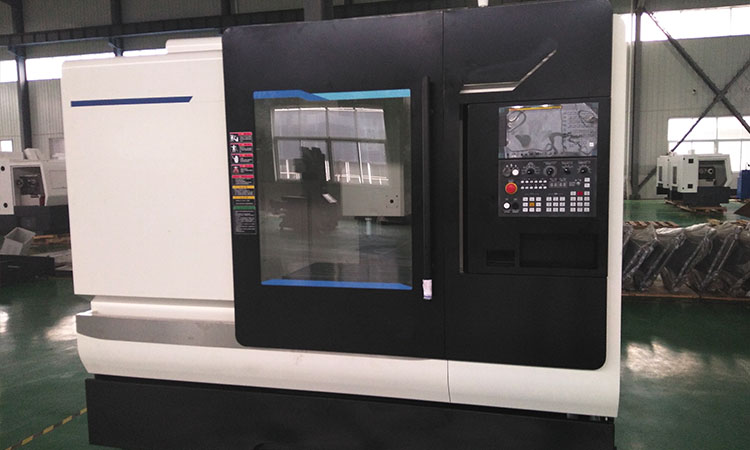
By definition, this is a computer numerical control lathe fitted with an automated material-handling system — bar stock feeding, chuck loading, or part unloading — so the spindle keeps cutting between cycles without waiting on an operator. The "automatic" part refers specifically to the loading and unloading function, not the cutting program itself, which is still CNC-controlled regardless of automation level. A standalone CNC lathe becomes an automatic CNC lathe once you bolt on a feeder, loader, or robot interface and integrate it with the machine's control signals.
Types of Automatic CNC Turning Lathes and Loading Systems
CNC lathe loading systems fall into six broad categories, each suited to a different stock format and output volume:
- Bar feeder — pushes long bar stock through the spindle bore for continuous unattended shaft and fitting production.
- Bar loader — loads short, pre-cut billets one at a time, useful when bar stock isn't practical.
- Gantry loader — an overhead pick-and-place unit that moves chucked parts between a raw stock tray, the machine, and a finished bin.
- Cobot (collaborative robot) — a compact arm that works alongside operators without full safety fencing, good for low-to-mid volume part changeovers.
- Robot cell — a fenced industrial robot arm with pallet or tray feeding, built for high-mix, high-volume, lights-out operation.
- Parts catcher — a mechanical arm or chute that simply retrieves finished parts from the spindle to protect surface finish, often paired with a bar feeder.
Some shops combine two of these — a bar feeder on a CNC inclined bed lathe plus a parts catcher, for example — to cover both continuous feeding and finish protection on precision shafts.
Comparing Six Automation Configurations by Part Type, Batch Size, and Operator Load
This is the comparison most buyers skip — and the one that causes the most expensive mistakes. Here's how the six configurations actually stack up on an automatic CNC lathe:
| Configuration | Best Part Type | Batch Size Fit | Cycle-Time Impact | Floor Space | Operator Requirement |
|---|---|---|---|---|---|
| Bar feeder | Shafts, pins, fittings from round/hex bar | High volume, long runs | Removes load/unload dead time almost entirely | Long footprint (bar length + feeder) | Periodic bar reload only |
| Bar loader | Short billets, pre-cut blanks | Medium volume | Adds a few seconds per cycle for indexing | Moderate, compact magazine | Magazine refill every few hours |
| Gantry loader | Chucked discs, flanges, housings | Medium to high volume, stable part mix | Fast, repeatable pick-and-place | Needs overhead clearance | Low — tray reload only |
| Cobot | Mixed small-to-medium parts, frequent changeovers | Low to medium, high mix | Slower than gantry but flexible across jobs | Small footprint, no fencing | Operator can work alongside it |
| Robot cell | Complex geometries, multi-operation parts | High volume, 24/7 runs | Fastest for multi-step, multi-machine tending | Large, fenced cell required | Minimal, mostly supervisory |
| Parts catcher | Finish-critical shafts and small turned parts | Any volume, used alongside a feeder | No cycle-time change, protects finish only | Minimal add-on | None beyond bin emptying |
What this table actually means in practice:
- Part type mismatch — running chucked flanges through a bar feeder simply doesn't work; the feeder needs continuous bar stock, so buyers who order one for disc-shaped parts end up with expensive dead equipment.
- Batch size misjudged — installing a robot cell for a 50-piece prototype run wastes capital that a gantry loader or even manual loading would have covered; robot cells only pay back on sustained volume.
- Floor space underestimated — bar feeders need clear floor length equal to the longest bar you'll run, often 3 meters or more; shops that skip this measurement end up with a feeder that can't be installed where planned.
- Operator requirement ignored — a cobot still needs someone to supervise fixture changes; treating it as fully unattended like a robot cell leads to missed quality checks.
Features of an Automatic CNC Turning Lathe Worth Checking Before You Order
Beyond the loading hardware, the base machine's build quality determines whether automation actually pays off. Look for a high-strength cast iron bed — resin sand casting with aging treatment holds dimensional accuracy over years of continuous cycles, which matters more on an automated line running unattended than on a manually tended lathe. Core transmission components — ballscrews and linear guideways — sourced from Taiwanese or German precision brands keep repeat-part tolerances consistent shift after shift. For mold-industry and other high-precision turning work, intelligent feedforward control and quadrant-protrusion compensation reduce the overcut marks, quadrant marks, and chatter lines that show up on parts run at automated speeds without an operator fine-tuning feed rates in real time. Machines capable of completing multiple faces in a single clamping also suit multi-variety, small-batch production, which pairs well with a CNC machining center for secondary operations when a single setup can't finish the part.
Automatic CNC Turning Lathe Applications
Automatic CNC lathes with bar feeders are standard on automotive fastener and fitting lines, where thousands of identical shafts or bushings run unattended overnight. Gantry-loaded lathes handle chucked components like pump housings and flange discs in mid-volume production. Cobots show up in job shops juggling five or six part numbers a week, where full robot tending isn't justified. Robot cells are common in mold and tooling component manufacturing, where a CNC turning center automation setup feeds a lathe and a secondary machining center in sequence for complex multi-face parts. Parts catchers protect finish-critical turned parts — bearing journals, precision pins — from scratching as they drop from the spindle.
Automatic CNC Turning Lathe Price and Cost Factors
Pricing on an automatic CNC turning lathe depends on the base machine spec, the automation hardware chosen, and order volume. Key cost drivers:
- Automation hardware — a bar feeder adds the least to total cost; a fenced robot cell adds the most due to safety guarding, vision systems, and integration labor.
- Batch purchase — there's no hard minimum order quantity; a single machine can be purchased, but ordering multiple units typically brings better pricing, lead time, or after-sales terms.
- Lead time — standard builds ship in 1 to 6 months depending on configuration and current production line load; stocked sample machines can move faster.
- Warranty scope — standard coverage is 12 months after acceptance with lifetime paid service available after; some tender projects specify extended coverage such as a 3-year free warranty, which affects quoted price.
- Customization — fixture design, bar capacity, or non-standard chuck interfaces for customized CNC machines add engineering time and cost versus an off-the-shelf configuration.
Automatic CNC Lathe Selection Checklist and Common Mistakes
Before requesting quotes, work through this checklist:
- Confirm your stock format — bar, billet, or pre-machined blank — this alone eliminates half the automation options.
- Calculate real batch size per part number over a 3-month window, not a single large order.
- Measure available floor length and overhead clearance where the machine will sit.
- Count how many part numbers run through the cell per week — high mix favors cobots or gantry loaders over bar feeders.
- Decide whether unattended overnight running is required; if so, a parts catcher or enclosed robot cell becomes necessary, not optional.
Common mistakes buyers make:
- Ordering a bar feeder sized for the wrong bar diameter or length, which then can't be retrofitted cheaply.
- Choosing a robot cell for prototype or short-run work where payback never materializes.
- Skipping a parts catcher on finish-critical shafts, then discovering scratched parts after the first unattended shift.
- Underestimating operator training time for cobot programming on frequent part changeovers.
Automatic CNC Turning Lathe Supplier Considerations
MAKCNC has operated multiple production lines since 2016, with sample machines in stock for buyers who need to inspect or trial a configuration before committing. Our facility is ISO9001:2015 certified, covering quality management across the build process. Standard warranty runs 12 months after acceptance with lifetime paid service afterward, and our after-sales network targets an 8-hour response with on-site support within 48 hours for machines already in the field. Production lead times run 1 to 6 months depending on the lathe spec and automation package ordered — there's no minimum order requirement, though multi-unit orders typically see better commercial terms on price or delivery. You can review our global case studies or read more about MAKCNC before reaching out with your part drawings.
FAQ on Automatic CNC Turning Lathes
Q: What's the difference between a bar feeder and a bar loader?
A: A bar feeder continuously pushes long bar stock through the spindle for unattended runs; a bar loader handles short, pre-cut billets one piece at a time, which suits parts that can't be made from continuous bar.
Q: Can I upgrade a manual-loading CNC lathe to add automation later?
A: It depends on spindle bore size, control interface, and available floor space — some machines are built automation-ready, others require retrofit work that's harder to justify after the fact.
Q: Do I need a robot cell for a low-mix, high-volume part?
A: Not necessarily. A bar feeder or gantry loader usually handles high-volume single-part runs more cost-effectively than a full robot cell, which is better justified by part complexity or multi-machine tending.
Q: Is there a minimum order quantity for an automatic CNC turning lathe?
A: No. A single unit can be purchased, though batch orders of multiple machines often come with better pricing or delivery terms.
If you're comparing automation configurations for your own part mix, send us your stock format, batch size, and target cycle time, or request a quotation and our team will recommend a loading setup that fits.